Accueil Outils et Consommables
Outils et Consommables
Durée de vie des électrodes de soudage et stockage
Pas de durée unique: dépend de la famille d'électrodes et du stockage. Conserver scellées et sèches; pour électrodes faible hydrogène, utiliser four/étuve; cons
Élodie Barbier 9 min de lecture
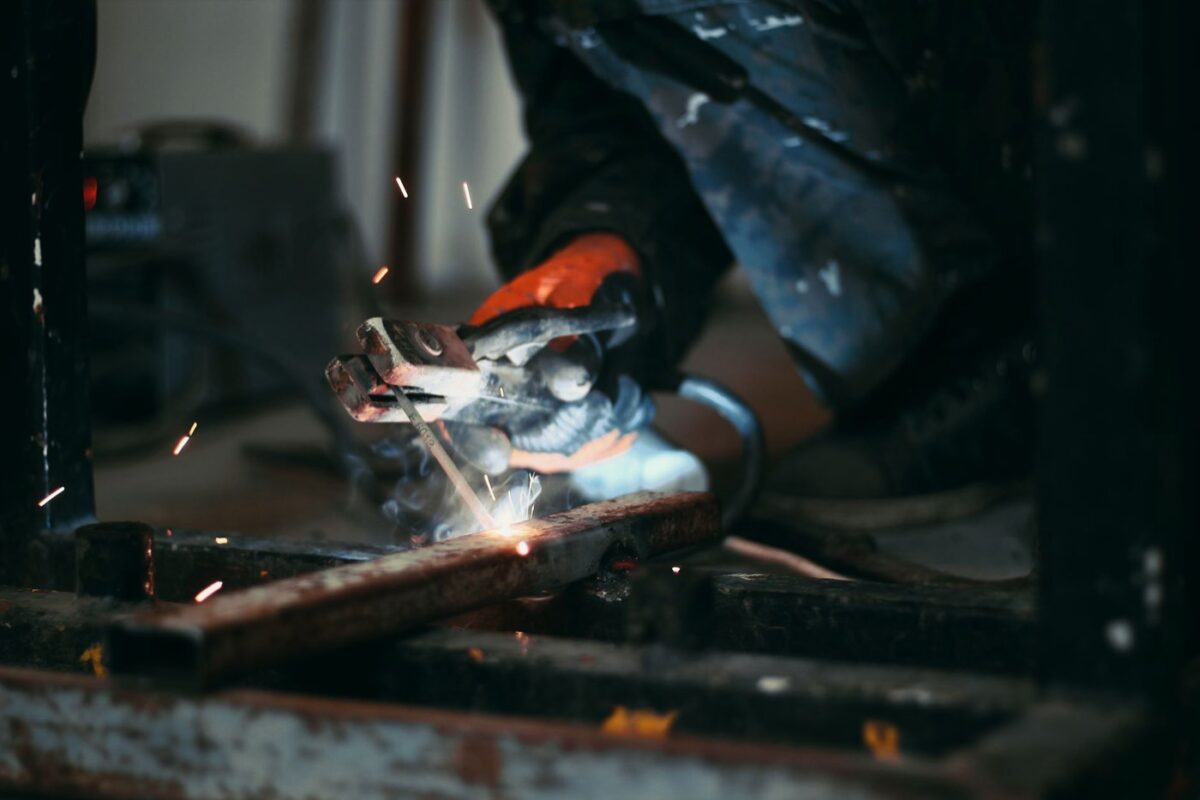
Short answer: there is no single shelf-life number for welding rods — longevity depends on electrode family and storage. Keep electrodes sealed and dry; use heated storage or rod ovens for moisture-sensitive low-hydrogen rods; consult AWS and the electrode manufacturer before re-drying or using exposed rods (see AWS guidance and manufacturer technical notes: https://studylib.net/doc/28461846/aws-a-5.5-a5.5m-2014; https://asremavad.com/wp-content/uploads/2018/10/AWS-D1.1-D1.1M-2015-Structural-Welding-Code%E2%80%94Steel-1.pdf; https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf, consulted 09/04/2026).
Why electrode storage matters
Covered electrodes absorb water from the atmosphere. Moisture in the flux coating changes the chemical balance at the arc and in the deposited weld metal; this increases the risk of hydrogen pickup and porosity, and for hydrogen-sensitive welds can raise the chance of cracking. Technical and standards guidance links moisture in coatings to degraded weld quality and prescribes storage and handling controls (AWS A5.5/A5.5M guidance and AWS D1.1 discussion: https://studylib.net/doc/28461846/aws-a-5.5-a5.5m-2014; https://asremavad.com/wp-content/uploads/2018/10/AWS-D1.1-D1.1M-2015-Structural-Welding-Code%E2%80%94Steel-1.pdf, consulted 09/04/2026).
Sensitivity to moisture differs by electrode family. Low-hydrogen electrodes (for example the E7018 family referenced in industry guidance) are intentionally produced with a coating chemistry that must remain dry; exposure requires controlled handling and, in many cases, oven storage after exposure (see low-hydrogen storage/handling guidance: https://www.welders-supply.com/welding-processes/stick-welding/7018-rod-storage-and-handling/, consulted 09/04/2026). Rutile and general-purpose coatings tolerate moisture to a greater degree than low-hydrogen coatings but will still see performance decline if left in humid conditions (CIGWELD technical pocket guide: https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf, consulted 09/04/2026).
Cellulosic electrodes behave differently: some cellulosic formulations rely on a certain moisture content for arc characteristics. That means drying and re-drying rules differ from low-hydrogen products and manufacturer guidance is the reference point for allowable treatment (TWI comparison of rutile vs cellulosic; Keen Ovens FAQs: https://www.twi-global.com/technical-knowledge/job-knowledge/comparison-of-the-use-of-rutile-and-cellulosic-electrodes-142; https://www.keenovens.com/resources/faqs, consulted 09/04/2026).
How long do welding rods last? Practical framing by type
Technical sources do not offer a universal « years » figure applicable to all electrodes; rather they tie usability to storage condition, packaging integrity, and electrode chemistry. Several industry guides note that unused electrodes in original sealed packaging and stored dry can remain usable for long periods, but the practical shelf life depends entirely on how they are stored and on the electrode family (WeldPundit; PakTechPoint: https://www.weldpundit.com/how-to-store-stick-electrodes-with-tips-for-home-welders/; https://paktechpoint.com/storage-of-welding-rods-and-electrodes/, consulted 09/04/2026).
- Low-hydrogen electrodes (E7XXX / E7018 family): High sensitivity to moisture; standards and manufacturer notes require controlled storage and specific handling if exposed. Follow AWS D1.1 and manufacturer instructions for exposure limits and conditioning (https://asremavad.com/wp-content/uploads/2018/10/AWS-D1.1-D1.1M-2015-Structural-Welding-Code%E2%80%94Steel-1.pdf; https://www.welders-supply.com/welding-processes/stick-welding/7018-rod-storage-and-handling/, consulted 09/04/2026).
- Rutile and basic coatings: More tolerant than low-hydrogen but still absorb moisture; keep sealed and dry and refer to manufacturer guidance before re-use after exposure (CIGWELD technical pocket guide: https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf, consulted 09/04/2026).
- Cellulosic electrodes: Different moisture behavior; drying procedures and storage rules are specific and in some cases cellulosic rods should not be stored long-term in a conventional rod oven unless the manufacturer allows it (TWI; Keen Ovens: https://www.twi-global.com/technical-knowledge/job-knowledge/comparison-of-the-use-of-rutile-and-cellulosic-electrodes-142; https://www.keenovens.com/resources/faqs, consulted 09/04/2026).
- Flux-cored wires and MIG/solid wires (including aluminum filler wire): Packaging and sealing are important. In humid environments heated cabinets or sealed storage are recommended; baking can remove moisture but may alter flux chemistry and is cautioned against without manufacturer advice (WPS Welding; AWS welding digest on aluminum storage: https://wpswelding.com/blog/fcaw-electrode-storage-moisture-control; https://www.aws.org/magazines-and-media/welding-digest/2025/august/wd-aug-2025-understanding-aluminum-storage-and-preparation, consulted 09/04/2026).
Recommended storage methods and temperatures
Common, standards-backed practices are: keep electrodes in their original sealed packaging until use; store in a dry location; use thermostatically controlled rod ovens or heated storage cabinets for moisture-sensitive electrodes; and limit exposure time during handling. These are cited across AWS guidance and manufacturer technical notes (https://studylib.net/doc/28461846/aws-a-5.5-a5.5m-2014; https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf, consulted 09/04/2026).
The briefed sources reference specific oven temperatures and handling categories, but those numerical parameters must be taken from the electrode manufacturer or the applicable AWS normative table before applying them to a given product. Do not use generic baking temperatures: consult the electrode technical data sheet or AWS normative guidance for the correct oven set points and timing for the product in question (AWS A5.5/A5.5M; manufacturer technical sheets: https://studylib.net/doc/28461846/aws-a-5.5-a5.5m-2014; https://www.nihonweld.com/images/items/uploads/NIHONWELD%20STORAGE%20%26%20HANDLING.pdf, consulted 09/04/2026).
Handling best practices include first-in/first-out rotation, limiting the time a batch is exposed on the bench, keeping boxes labeled with date received and oven history for code work, and storing in a controlled cabinet if ambient humidity is high (CIGWELD; PakTechPoint: https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf; https://paktechpoint.com/storage-of-welding-rods-and-electrodes/, consulted 09/04/2026).
What to do if rods have been exposed (reconditioning / baking)
First, assess visually for rust, soft or swollen coatings, grease, or obvious wetness. Manufacturers and technical guides advise discarding visibly damaged rods or following manufacturer-specific reconditioning procedures (CIGWELD technical pocket guide: https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf, consulted 09/04/2026).
If a product’s technical data sheet or AWS normative tables specify re-drying parameters, follow those exact temperatures and times. Several references warn that re-baking can alter flux chemistry—particularly for flux-cored wires—and that unpredictable changes to welding behavior can result without manufacturer approval (WPS Welding; AASHTO/AWS commentary: https://wpswelding.com/blog/fcaw-electrode-storage-moisture-control; https://www.rexresearch1.com/WeldingLibrary/BridgeWeldingCode.pdf, consulted 09/04/2026).
When code-controlled work is involved, document any reconditioning and ensure procedures match AWS or project specifications. If no manufacturer or code-approved procedure exists for a product, do not assume generic baking will restore it — consult the manufacturer.
Signs an electrode is no longer usable
Visual signs: visible rust, flaking or softened flux coating, wet sheen, or a badly degraded label and packaging are cues to reject or to consult the manufacturer. Performance signs: unstable arc, excessive spatter, or porosity in test welds indicate moisture-damaged electrodes. Technical guides recommend test welds on scrap when doubt exists and consulting the electrode TDS or manufacturer for disposition (CIGWELD technical pocket guide; WeldPundit: https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf; https://www.weldpundit.com/how-to-store-stick-electrodes-with-tips-for-home-welders/, consulted 09/04/2026).
Special cases and project-critical rules
For structural welding governed by codes such as AWS D1.1, storage, exposure time, and conditioning are not optional. AWS D1.1 and related normative guidance set requirements and limits for low-hydrogen electrodes and expect documented handling for project acceptance; follow the code text and the electrode manufacturer precisely when working on code-controlled assemblies (AWS D1.1/D1.1M: https://asremavad.com/wp-content/uploads/2018/10/AWS-D1.1-D1.1M-2015-Structural-Welding-Code%E2%80%94Steel-1.pdf; AASHTO/AWS commentary: https://www.rexresearch1.com/WeldingLibrary/BridgeWeldingCode.pdf, consulted 09/04/2026).
For cellulosic electrodes, manufacturer guidance and specialized references (TWI; Keen Ovens) should drive decisions about oven use and drying. Some cellulosic rods can be negatively affected by standard rod oven programs unless the manufacturer explicitly permits such conditioning (https://www.twi-global.com/technical-knowledge/job-knowledge/comparison-of-the-use-of-rutile-and-cellulosic-electrodes-142; https://www.keenovens.com/resources/faqs, consulted 09/04/2026).
Quick checklist for workshop managers
- Store electrodes in original sealed packaging and control ambient humidity (manufacturer and AWS guidance: https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf; https://studylib.net/doc/28461846/aws-a-5.5-a5.5m-2014, consulted 09/04/2026).
- Use rod ovens or heated cabinets for moisture-sensitive electrodes and follow manufacturer or AWS temperature/time parameters when specified (see AWS and manufacturer guidance: https://studylib.net/doc/28461846/aws-a-5.5-a5.5m-2014; https://www.keenovens.com/resources/faqs, consulted 09/04/2026).
- Label boxes with receipt date and oven history; rotate stock FIFO for quality control (CIGWELD; PakTechPoint: https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf; https://paktechpoint.com/storage-of-welding-rods-and-electrodes/, consulted 09/04/2026).
- Visually inspect batches before use and perform test welds on scrap when in doubt (WeldPundit: https://www.weldpundit.com/how-to-store-stick-electrodes-with-tips-for-home-welders/, consulted 09/04/2026).
- For project- or code-controlled welding, document storage and any reconditioning per AWS D1.1 and manufacturer instructions (AWS D1.1: https://asremavad.com/wp-content/uploads/2018/10/AWS-D1.1-D1.1M-2015-Structural-Welding-Code%E2%80%94Steel-1.pdf; AASHTO/AWS commentary: https://www.rexresearch1.com/WeldingLibrary/BridgeWeldingCode.pdf, consulted 09/04/2026).
Further reading & standards (links)
- AWS A5.5 / A5.5M storage and handling guidance — reference copy: https://studylib.net/doc/28461846/aws-a-5.5-a5.5m-2014 (consulted 09/04/2026).
- AWS D1.1 / D1.1M Structural Welding Code — Steel (exposure and conditioning requirements): https://asremavad.com/wp-content/uploads/2018/10/AWS-D1.1-D1.1M-2015-Structural-Welding-Code%E2%80%94Steel-1.pdf (consulted 09/04/2026).
- CIGWELD Technical Pocket Guide — storage and conditioning: https://www.cigweld.com.au/wp-content/uploads/elementor/forms/CIG-7024-CIGWELD-Technical-Pocket-Guide-v2.pdf (consulted 09/04/2026).
- TWI summary on rutile vs cellulosic electrodes: https://www.twi-global.com/technical-knowledge/job-knowledge/comparison-of-the-use-of-rutile-and-cellulosic-electrodes-142 (consulted 09/04/2026).
- Manufacturer and industry practical guides referenced above (WeldPundit, PakTechPoint, WPS Welding, Keen Ovens, NIHONWELD): see source list in this article (all consulted 09/04/2026).
What we don’t know / when to contact the manufacturer
This article does not provide a universal numeric shelf-life in years for all welding rods; no manufacturer-specific expiry dates or guaranteed lifespans were provided in the materials used to compile this guide. Exact oven temperatures, exposure-time limits, and allowable re-drying cycles for a specific product are not listed here unless taken directly from that product’s technical documentation. For a given electrode or wire, consult the product technical data sheet (TDS) or the manufacturer before applying drying parameters or accepting reconditioned material. If the work is code-governed, follow AWS D1.1 and the electrode manufacturer’s instructions exactly and document any reconditioning (https://asremavad.com/wp-content/uploads/2018/10/AWS-D1.1-D1.1M-2015-Structural-Welding-Code%E2%80%94Steel-1.pdf; https://studylib.net/doc/28461846/aws-a-5.5-a5.5m-2014, consulted 09/04/2026).
Note: no proprietary data bank or site-specific voice file was available in the brief at the time of drafting (DATA-BANK.md and VOICE.md were not provided). Add product TDS or manufacturer technical sheets to the project folder if available to allow insertion of product-specific shelf-life and oven parameters.
Image alt text suggestions
- Heated rod oven with sealed boxes of electrodes — alt: « Heated rod oven with sealed electrode boxes. »
- Dry storage cabinet with labeled electrode boxes — alt: « Dry storage cabinet holding labeled welding rod boxes. »
- Inspection of welding rod coating — alt: « Close-up of electrode coating showing rust and degradation. »
Rédactrice · travaux, rénovation, matériaux
Élodie se concentre sur les techniques de rénovation et l'utilisation des matériaux innovants. Elle s'assure de la véracité des contenus en se basant sur des études et des témoignages d'experts avant publication.
Dans Outils et Consommables
16 septembre 2026
New Plasma Power Source: A Game Changer for Home Metal Fabrication
15 septembre 2026
Features of the Grizzly Horizontal Miter-Cutting Band Saw
15 septembre 2026